What we machine for industry
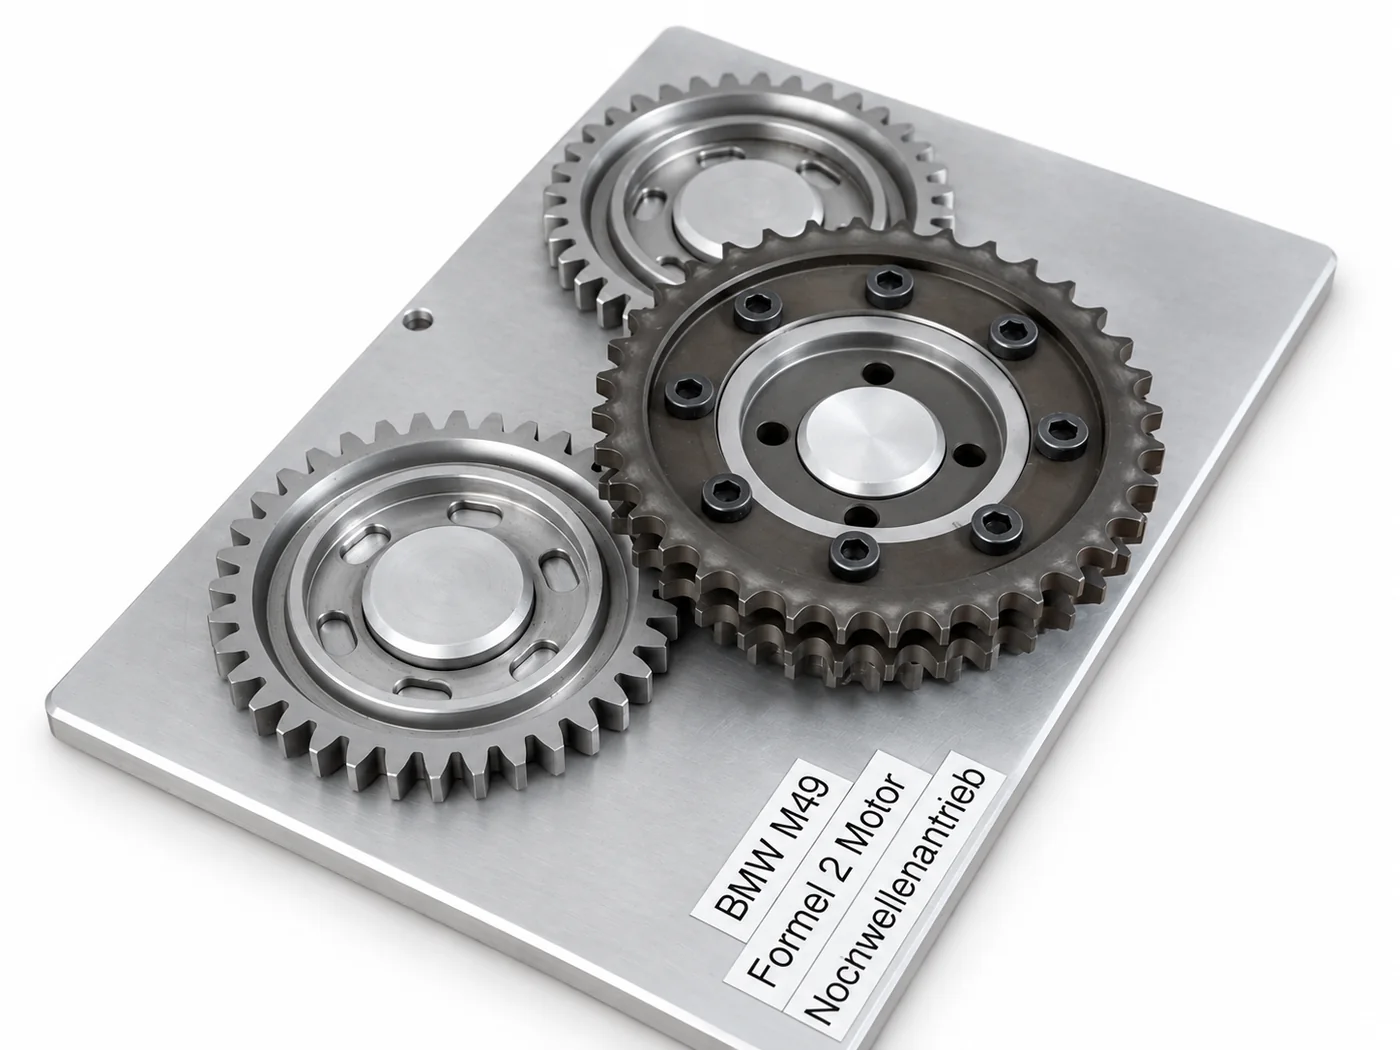
Our core business for industrial customers is ready-to-install turned and gear-cut parts in early development phases:
Prototype parts for drivetrains and assemblies
Shafts, gears, spline profiles and special parts in the early development phase. Typically these are components that do not exist as standard or catalogue parts and are needed for test mules, rig builds or concept vehicles – from batch size 1, to drawing or sample.First-sample parts
The stage before production release. A first sample has to show that drawing and process fit together – so we deliver it measured and documented, with a measurement report if your quality assurance requires one.Small series
When production tooling does not yet exist or does not pay off at that quantity. We machine without the tooling cost block that makes small series uneconomical at volume suppliers – and repeatably, because drawing and settings stay documented.Turned and gear-cut parts for construction and agricultural machinery
And for general mechanical engineering. Usually this is about replacing parts the manufacturer no longer lists or only supplies with long lead times – gears, shafts and sprockets are made anew from the old part so the machine runs again.
Producing first samples, prototypes and small series is not a sideline next to volume work here – it is what the workshop is built around. One part, one drawing, one binding deadline.
One workshop, every operation
Prototype parts rarely fail at the lathe – they fail at the interface between trades. So we keep the chain in-house:
Drawing creation in DWG/DXF format
Including from sample parts. If only a worn original exists, we measure it, reconstruct the nominal dimensions and gear data, and produce the manufacturing drawing. The design data is yours afterwards.CNC and conventional turning up to 600 mm diameter
CNC-controlled on the Seiler SLZ 570 with Heidenhain control, conventional up to 1800 mm turning length. That covers long shafts smaller workshops have to turn away.Internal and external gear cutting up to 500 mm diameter and module 8
Straight and helical, on our own shaping and hobbing machines. This operation is exactly what separates us from a plain turning shop – it stays in-house instead of being bought in.Keyway slotting and broaching, spline profiles
Internal keyways up to 32 mm width and 200 mm length. A cleanly broached keyway sits without play – under alternating loads that is exactly what decides whether the joint holds or hammers out.TIG welding of steel, stainless steel and aluminium
Low-distortion and machinable afterwards – important when the part still needs fitting dimensions. Welding and finish machining run in the same order here.Laser-cut parts and surface finishing
water blasting and magnesium pickling in-house, plating, powder coating and painting with proven partners. You receive a finished component, not a raw blank – cutting, machining and finishing from one source, with no supplier chain for you to coordinate.
Precision with proof
Gear teeth are ground to tolerances down to the region of 0.0025 mm – with a measurement report if your quality assurance requires it. Bearing friction torque is set using a torsiometer with drag indicator. First samples that leave this workshop are measured, not estimated.
Discretion goes without saying
Development parts are confidential. Drawings, samples and project data stay in-house and are not mentioned to third parties – we will confirm that in writing on request.