Production programme
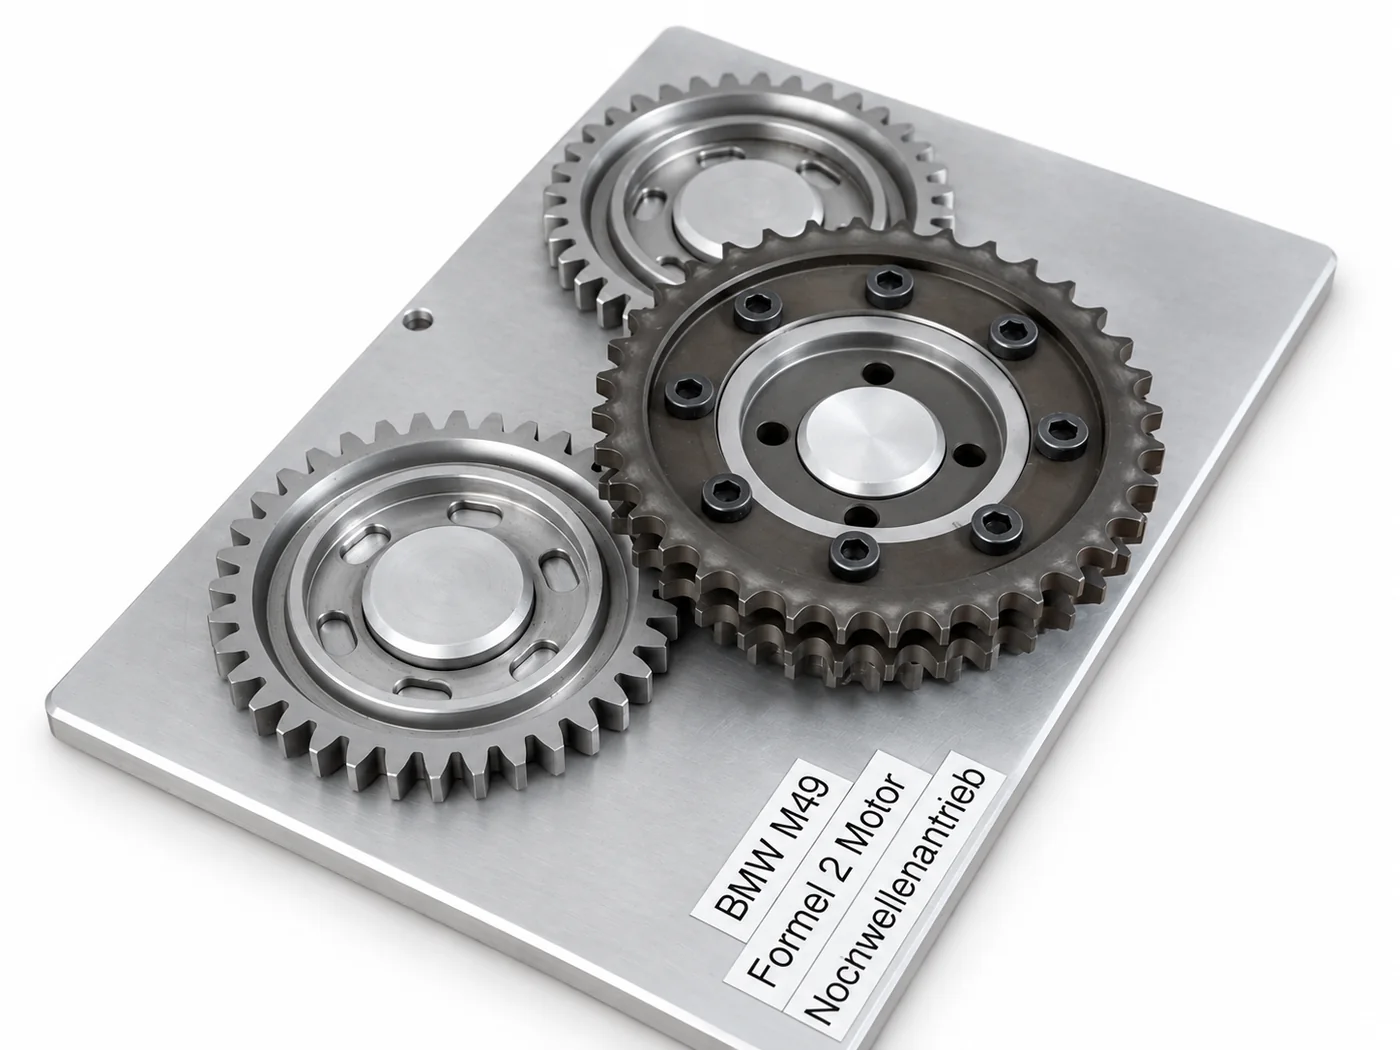
On our turning and gear-cutting machines we produce:
CNC-turned parts up to 500 mm turning diameter
On the Seiler SLZ 570 with Heidenhain control, workpieces up to 500 kg between centres. Conventionally we turn up to 600 mm diameter and 1800 mm length.Gears, straight and helical cut
Internal and external, up to 500 mm diameter and module 8. Helical teeth run quieter and carry more load but generate axial forces – which variant fits is settled from the installation and the bearing arrangement.Special tooth profiles to drawing or sample
Including profiles for which no standard tooling exists – we then have the matching tool made as a special. Your job does not fail at our tool cabinet.Sprockets up to 500 mm diameter
Including valve-train sprockets for classic engines, where original parts disappeared long ago. Made from a sample, with correct pitch and tooth form so the chain runs cleanly.Splined shafts and spline profiles
Internal keyways slotted or broached up to 32 mm width and 200 mm length. The operation most workshops have to buy in – here the machine stands in our own shop.Gearbox shafts up to 800 mm length
Straight or helical cut, machined from a single billet and heat-treated. For racing gearboxes with ground teeth and a measurement report on request.Replacement parts for discontinued gearbox components
Also from manufacturers other than Porsche. When a gear or shaft has been out of production for decades, the old part is the pattern – measured, drawn, made new.
We keep an extensive stock of standard tooling plus a large number of special tools from the automotive industry. If a profile is missing, we have the matching tool made as a special – your job does not fail at the tool cabinet.
From old part to drawing to new part
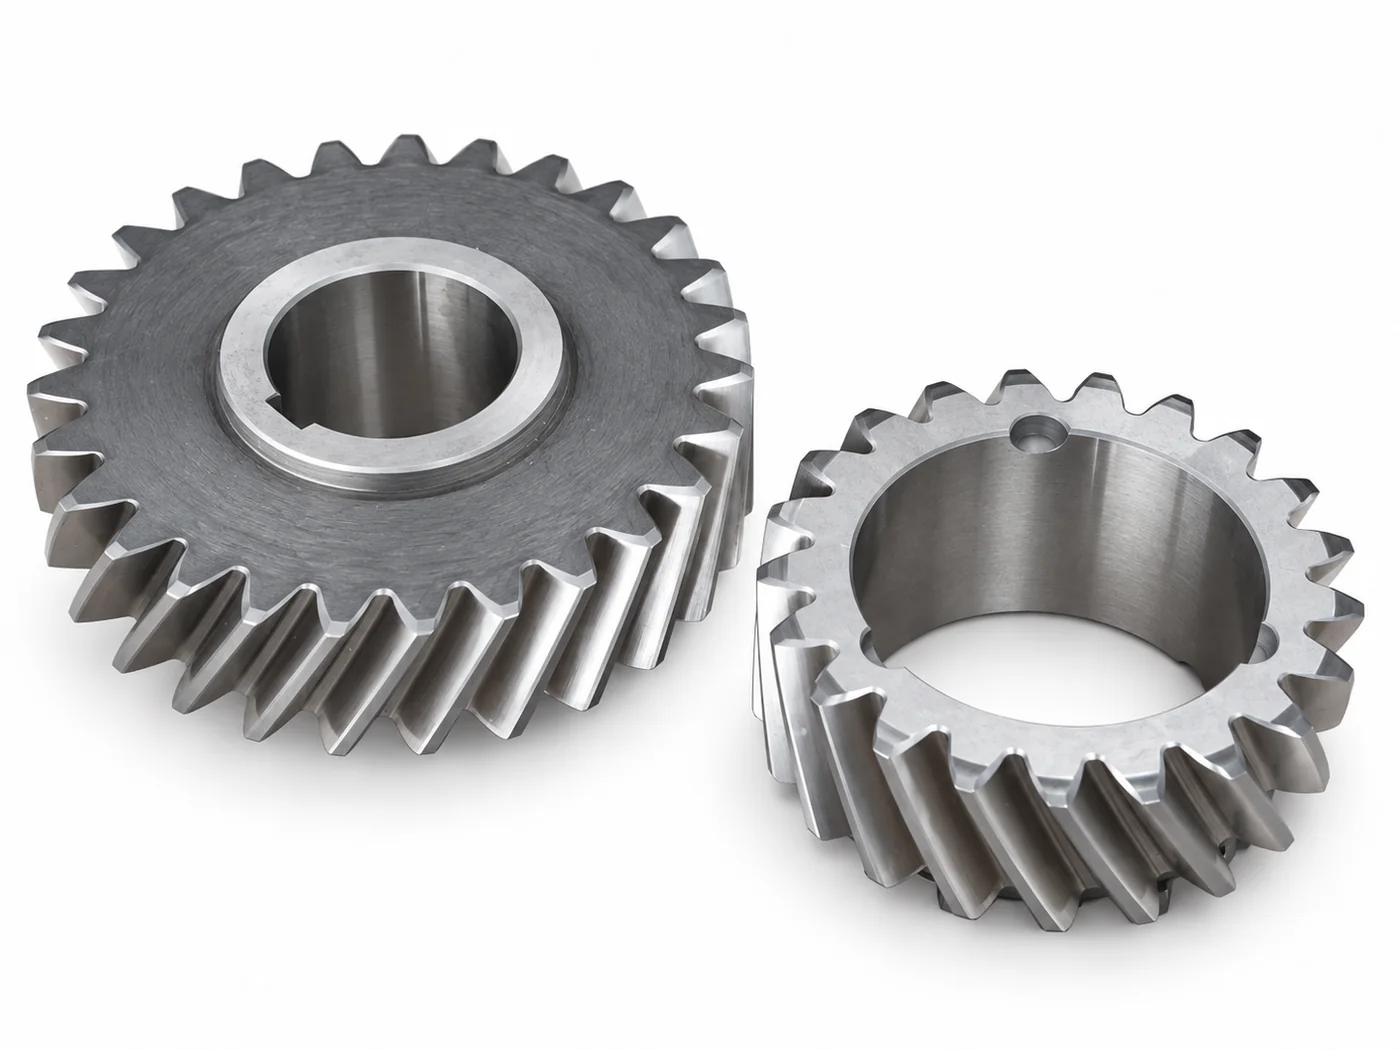
The most common case: only the worn or broken original still exists. We measure the sample, determine module, pressure angle and corrections, create the CAD drawing in DWG/DXF format and machine the new part – one point of contact from the first measurement to the ready-to-install component.
Machining to your drawing
Restorers, workshops and machine builders use us as their extended workbench:
Turning, milling and drilling to drawing
When your own capacity is short or the part is too large for your machines. Deadlines are committed, not estimated.Keyway slotting and broaching up to 32 mm width
Key seats, keyways and internal profiles in hubs, gears, pulleys and flanges. Single pieces too, even though broaching is otherwise a series process.TIG welding of steel, stainless steel and aluminium
Clean and low-distortion, so the part can still be machined to size afterwards. Typical jobs are cracked brackets and housing sections on classic cars.Laser-cut parts and surface finishing
water blasting and magnesium pickling in our own workshop; plating, powder coating and painting organised with proven partners – all from one source. On restored cars the faithful original appearance usually matters more than gloss; we match the finish to that.
Quality you can measure
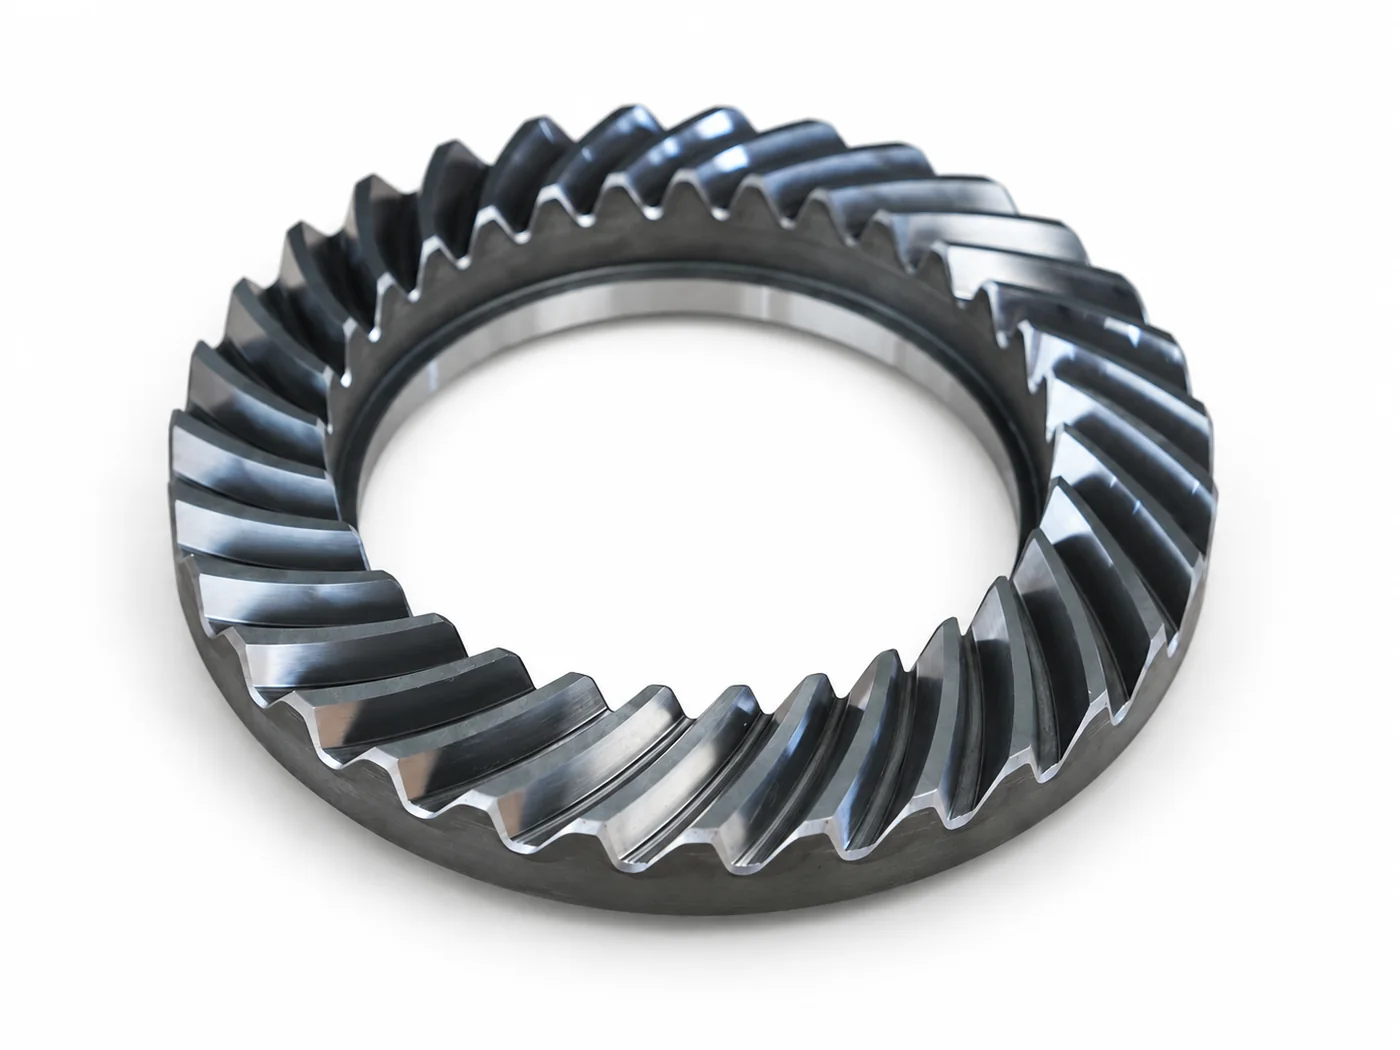
Gear quality is not a promise, it is a measured value. Ground gear teeth are produced with tolerances down to the region of 0.0025 mm – with a measurement report for the part on request.